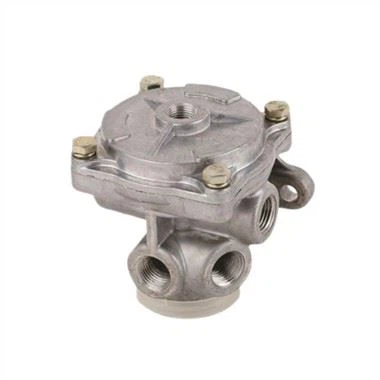
In mining operations, air master booster failures cause 18% of unplanned downtime (Global Mining Report 2023), costing up to $15,000 per hour in lost productivity. This guide details Xinlida's proven 3-tier inspection protocol for Cat 797F, Komatsu 980E, and other ultra-class haul trucks, proven to reduce booster-related breakdowns by 67%.
Why Mining Demands Aggressive Inspection Schedules
Harsh Operating Conditions:
Particulate Load: 200–300 mg/m³ dust concentrations (ISO 12103-1 Grade C)
Payload Stress: 400+ tons GVWR induces 5G vibration forces
Thermal Cycling: -30°C to 120°C daily swings in open-pit mines
Failure Statistics:
55% of air booster failures originate from contaminated valves
30% result from seal degradation in high-heat environments
Xinlida's 3-Tier Inspection Protocol
Tier 1: Daily Visual Checks (5–7 Minutes)
Air Pressure Gauge Verification:
Target: 110–125 psi (7.6–8.6 bar)
Tolerance: ±5 psi variation indicates regulator issues
External Leak Detection:
Apply soap solution to fittings – bubbles reveal leaks
Ultrasonic detector (40 kHz+) for micro-leaks <0.5 CFM
Dust Cap Integrity:
Inspect Xinlida's cyclone pre-filters for blockage (replace if >30% covered)
Tool Kit Requirement:
Digital pressure gauge (0.1 psi resolution)
Infrared thermometer (measure housing temp differentials)
Tier 2: Monthly Performance Tests (1–2 Hours)
Pushrod Stroke Measurement:
Specification: 2.3–2.8 inches (58–71 mm)
Excessive travel (>3") indicates diaphragm wear
Response Time Analysis:
Healthy System: 0.25–0.35 sec from pedal press to full boost
Degraded Performance: >0.5 sec requires valve cleaning
Contamination Check:
Drain air reservoir – permissible water content <1 oz/day
Submit oil samples for ISO 4406 particle count
Case Study:
A Chilean copper mine extended booster lifespan by 40% through monthly ISO cleanliness code tracking.
Tier 3: Annual Overhaul (8–12 Hours)
Full Disassembly & Cleaning:
Ultrasonic bath for valve blocks (30 min @ 40 kHz)
Replace Xinlida's wear-and-tear kit (P/N: XLD-MTK-45)
Material Integrity Tests:
Magnetic particle inspection for housing cracks
Shore A hardness testing of HNBR seals (min 70A)
Dynamometer Simulation:
500,000 pressure cycles @ 12 bar (simulates 5-year service)
Critical Replacement Intervals
| Component | Mining Duty Cycle | Replacement Interval |
|---|---|---|
| Diaphragm | 24/7 Operation | 18–24 Months |
| Valve Seats | High-Silica Environments | 12 Months |
| Dust Pre-Filter | Dry Iron Ore Mines | 6 Months |
| Housing Assembly | Ultra-Class Haulers | 5 Years |